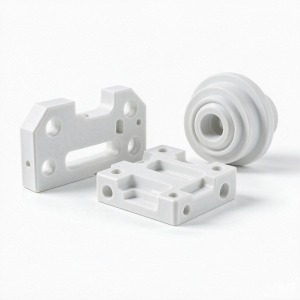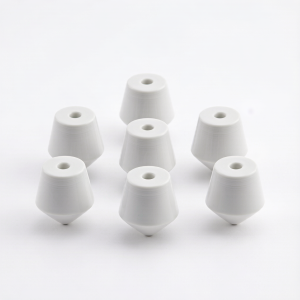
Ceramic nozzles meter, direct or atomise a fluid, a gas or an abrasive stream. The orifice is the whole point of the part.
Silicon carbide nozzles are the standard for abrasive blasting and slurry spraying. They resist the erosive wear that opens a steel orifice within hours, and the high conductivity helps them survive in burner and torch applications.
Silicon carbide is chosen when a part must survive abrasion, high temperature and thermal shock at the same time. Hardness reaches 2200-2500 HV, thermal conductivity of 120-200 W/m·K is several times that of steel, and expansion of 4.0 ×10⁻⁶/K keeps it in shape through fast temperature swings.
It is brittle and electrically semiconducting, so it is not used where electrical isolation matters, and its hardness makes diamond grinding the only practical finishing route.
Specifications
| Orifice diameter | 0.1-10 mm |
| Orifice tolerance | ±0.005 mm |
| Outer diameter | 5-60 mm |
| Length | up to 150 mm |
| Orifice concentricity | 0.01 mm |
| Bore finish | Ra 0.4 µm |
| Entry | radiused, conical or sharp edge |
Silicon Carbide Properties
| Composition | Sintered silicon carbide (SSiC) |
| Density | 3.10-3.15 g/cm³ |
| Vickers hardness | 2200-2500 HV |
| Flexural strength | 400-500 MPa |
| Fracture toughness | 3-4 MPa·m½ |
| Max. service temperature | 1400°C in air (1600°C inert) |
| Thermal conductivity | 120-200 W/m·K |
| Thermal expansion (20-1000°C) | 4.0 ×10⁻⁶/K |
Machining and Tolerances
Nozzles are turned and ground from solid stock rather than cast, because bore and outside have to be concentric. Orifices below about 0.5 mm are produced by precision drilling or laser, and the entry is radiused rather than sharp so the flow does not separate.
Where It Is Used
- Abrasive blasting and slurry spray nozzles
- Burner and plasma torch nozzles
- Atomising nozzles for coating and humidification
- Precision dispensing tips in fluid handling
- High-wear spray tips in scrubber and desulphurisation systems
Frequently Asked Questions
How small an orifice can you produce?
Down to about 0.1 mm depending on material and length. Small deep holes are the hardest features to hold, so we normally discuss the length-to-diameter ratio before quoting.
Which material wears longest in abrasive service?
Boron carbide then silicon carbide for pure abrasion, and silicon nitride where impact and thermal shock are present too. We match the material to the abrasive, the velocity and the fluid rather than defaulting to the hardest option.