


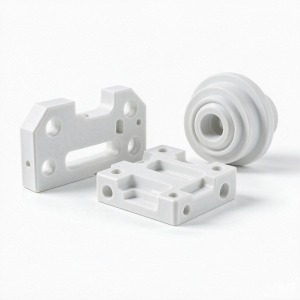
Custom Silicon Carbide Ceramic Parts are made to your drawing rather than to a catalogue shape: complex outlines, intersecting bores, thin walls and asymmetrical features that no standard shape covers.
Custom silicon carbide parts are made for the hardest duties, combining abrasion, high temperature and corrosion. The material is expensive to grind, so we confirm that the duty justifies it before quoting.
Silicon carbide is chosen when a part must survive abrasion, high temperature and thermal shock at the same time. Hardness reaches 2200-2500 HV, thermal conductivity of 120-200 W/m·K is several times that of steel, and expansion of 4.0 ×10⁻⁶/K keeps it in shape through fast temperature swings.
It is brittle and electrically semiconducting, so it is not used where electrical isolation matters, and its hardness makes diamond grinding the only practical finishing route.
Specifications
| Process route | pressing, CIP, injection moulding or extrusion |
| Finishing | diamond grinding, lapping, honing |
| Dimensional tolerance | ±0.01 mm, ±0.002 mm on ground features |
| Surface finish | Ra 0.4 µm ground, Ra 0.05 µm polished |
| Features | bores, slots, threads, tapers, pockets |
| Quantity | single prototypes to production volumes |
| Drawing formats | DXF, STEP, IGES, PDF |
Silicon Carbide Properties
| Composition | Sintered silicon carbide (SSiC) |
| Density | 3.10-3.15 g/cm³ |
| Vickers hardness | 2200-2500 HV |
| Flexural strength | 400-500 MPa |
| Fracture toughness | 3-4 MPa·m½ |
| Max. service temperature | 1400°C in air (1600°C inert) |
| Thermal conductivity | 120-200 W/m·K |
| Thermal expansion (20-1000°C) | 4.0 ×10⁻⁶/K |
Machining and Tolerances
Complex parts are near-net shaped by pressing, injection moulding or isostatic pressing, then ground with diamond tooling to the finished features. Green machining before firing is used where it saves grinding time, and we always advise on which features are worth holding and which will drive cost without adding function.
Where It Is Used
- Semiconductor and vacuum equipment components
- Fixtures and nests for welding, brazing and assembly
- Analytical and medical instrument parts
- Wear components for packaging and converting machinery
- High-voltage and high-frequency insulators
Frequently Asked Questions
What tolerance should I put on the drawing?
Hold tolerance only on features that matter. A blanket ±0.01 mm across a complex part can double or treble the cost without improving function, so we mark the functional features and leave the rest open.
Can you help with the design before quoting?
Yes, and it usually saves money. We review draft geometry for wall thickness, sharp corners and features that will not grind cleanly, then suggest changes before the drawing is frozen.