


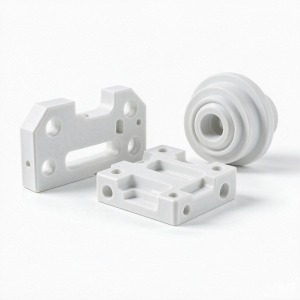
Custom Fused Silica Ceramic Parts are made to your drawing rather than to a catalogue shape: complex outlines, intersecting bores, thin walls and asymmetrical features that no standard shape covers.
Custom fused silica parts are made for UV optics, viewports and components exposed to extreme thermal cycling. The near-zero expansion allows shapes that would crack in any other ceramic.
Fused silica expands by only 0.5 ×10⁻⁶/K, so it can go from red heat to cold water without cracking. It is an excellent electrical insulator, transmits UV, and its amorphous structure gives a very smooth non-porous surface.
Strength is low for a ceramic at 50-70 MPa and the material is relatively soft. Above 1000°C it starts to devitrify, losing both transparency and thermal shock resistance.
Specifications
| Process route | pressing, CIP, injection moulding or extrusion |
| Finishing | diamond grinding, lapping, honing |
| Dimensional tolerance | ±0.01 mm, ±0.002 mm on ground features |
| Surface finish | Ra 0.4 µm ground, Ra 0.05 µm polished |
| Features | bores, slots, threads, tapers, pockets |
| Quantity | single prototypes to production volumes |
| Drawing formats | DXF, STEP, IGES, PDF |
Fused Silica Properties
| Composition | Amorphous silicon dioxide |
| Density | 2.20 g/cm³ |
| Vickers hardness | 600-800 HV |
| Flexural strength | 50-70 MPa |
| Fracture toughness | 0.7-1.0 MPa·m½ |
| Max. service temperature | 1000°C (1200°C short term) |
| Thermal conductivity | 1.4 W/m·K |
| Thermal expansion (20-1000°C) | 0.5 ×10⁻⁶/K |
Machining and Tolerances
Complex parts are near-net shaped by pressing, injection moulding or isostatic pressing, then ground with diamond tooling to the finished features. Green machining before firing is used where it saves grinding time, and we always advise on which features are worth holding and which will drive cost without adding function.
Where It Is Used
- Semiconductor and vacuum equipment components
- Fixtures and nests for welding, brazing and assembly
- Analytical and medical instrument parts
- Wear components for packaging and converting machinery
- High-voltage and high-frequency insulators
Frequently Asked Questions
What tolerance should I put on the drawing?
Hold tolerance only on features that matter. A blanket ±0.01 mm across a complex part can double or treble the cost without improving function, so we mark the functional features and leave the rest open.
Can you help with the design before quoting?
Yes, and it usually saves money. We review draft geometry for wall thickness, sharp corners and features that will not grind cleanly, then suggest changes before the drawing is frozen.